Valve-regulated lead-acid (VRLA) batteries have become indispensable in modern energy storage applications, ranging from telecommunications base stations and uninterruptible power supplies to automotive start-stop systems and renewable energy storage. The global market for AGM separators, a critical component of these batteries, reached approximately 1,058 million square meters in 2025 and continues to grow steadily . At the heart of every VRLA battery lies the absorptive glass mat (AGM) separator—a seemingly simple fibrous material that performs a complex array of electrochemical, mechanical, and transport functions. Choosing the wrong separator can lead to premature capacity loss, electrolyte stratification, thermal runaway, or catastrophic battery failure. This article provides a comprehensive guide to selecting the optimal AGM separator for VRLA battery applications.
The Critical Functions of an AGM Separator
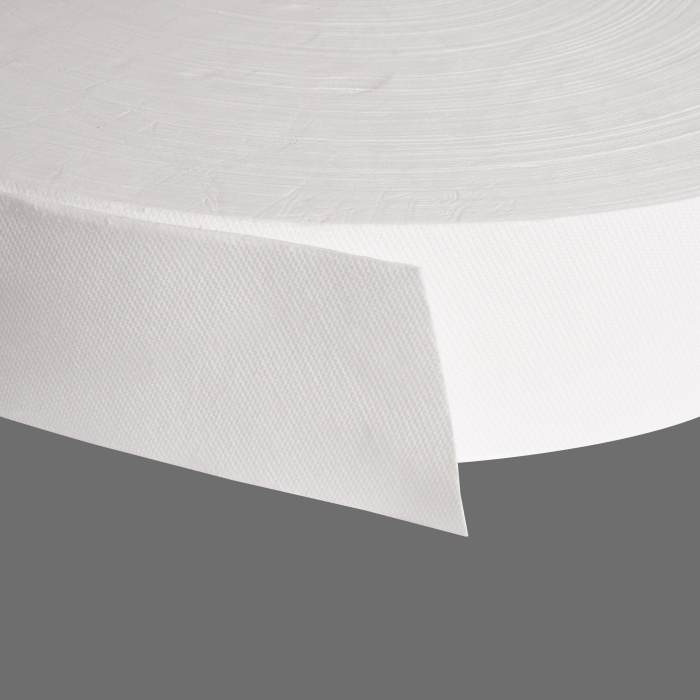
Before examining selection criteria, it is essential to understand what the AGM separator must accomplish. Unlike flooded lead-acid batteries where the separator primarily prevents short circuits, the AGM separator in a VRLA cell performs multiple simultaneous functions that directly determine battery performance and longevity.
The most fundamental function is physical separation—preventing direct contact between positive and negative plates that would cause short circuits . However, this is merely the baseline. The separator must also serve as an electrolyte reservoir, absorbing and retaining the sulfuric acid that enables ionic conduction between plates. In VRLA designs, the electrolyte is immobilized within the separator’s pore structure rather than freely flooding the cell.
A uniquely critical function is facilitating the oxygen recombination cycle. In VRLA batteries, oxygen generated at the positive plate during charging must migrate to the negative plate where it recombines to form water. The AGM separator must maintain a network of gas channels—typically about 5-10% of its pore volume—while remaining 90-95% saturated with electrolyte . This delicate balance between liquid retention and gas permeability distinguishes AGM technology from all other battery separator types.
Finally, the separator must maintain compression on the plate group throughout the battery’s life. As positive plates grow and shed active material during cycling, the separator must exert consistent pressure to preserve good electrical contact and minimize capacity loss .
Key Selection Criteria
Fiber Composition and Pore Structure
The performance characteristics of an AGM separator are fundamentally determined by its fiber composition. AGM separators are manufactured from glass microfibers, typically with diameters ranging from 0.1 to 10 micrometers, through a papermaking-like wet process . The ratio of fine fibers (diameter less than 1 micrometer) to coarse fibers (approximately 3 micrometers) is the primary lever for tailoring separator properties.
Fine fibers increase the internal surface area and reduce pore diameter, which enhances capillary pressure and electrolyte retention . However, fine fibers also increase cost and can reduce tensile strength. Coarse fibers create larger pores that facilitate acid filling and oxygen transport but may compromise electrolyte uniformity. The relationship between fiber content and capillary pressure follows the Laplace equation, where capillary pressure is inversely proportional to pore radius . By adjusting the proportion of fine to coarse fibers, manufacturers can produce AGM materials with precisely defined pore size distributions.
A typical optimized formulation for VRLA separators contains 20-40% by weight of microfibers with diameters below 1 micrometer and 60-80% coarse fibers with diameters around 3 micrometers . The resulting pore structure should exhibit a median pore diameter in the range of 5-8 micrometers for optimal performance .
Thickness and Compression Behavior
AGM separator thickness is quoted under a controlled standard pressure of 10 kPa, but the in-cell thickness is substantially less due to compression . During battery assembly, plate groups are compressed to reduce separator thickness by approximately 25%, ensuring intimate contact between the separator and active materials . This compression is critical for maintaining ionic conductivity and mechanical stability.
Thickness requirements vary significantly by application. For automotive start-stop batteries, AGM layers typically range from 0.1 to 1.1 mm, while industrial and stationary battery separators are considerably thicker, ranging from 0.5 to 3.1 mm . The appropriate thickness depends on the space available in the cell, the required acid volume, and the compression force needed to maintain plate contact.
Wet elasticity—the ability of the separator to maintain compression even when saturated with electrolyte—is a critical but often overlooked property. Research has shown that plate-group pressure caused by separator elasticity is strongly effective in suppressing capacity loss during deep cycling . Separators with higher fine fiber content generally exhibit better wet resilience, though this must be balanced against cost and acid filling considerations.
Electrolyte Absorption and Wicking Properties
The separator’s ability to rapidly absorb and uniformly distribute sulfuric acid during filling and throughout battery life is essential for manufacturing efficiency and performance consistency . Acid wicking rates are typically measured in millimeters per two minutes, with commercial AGM separators exhibiting values ranging from approximately 60 to 67 mm/2min .
Specific surface area, commonly measured using the BET method, is a key indicator of wicking performance. Commercial AGM separators typically exhibit BET values between 0.8 and 2.0 m²/g . Higher surface area generally correlates with faster wicking and better electrolyte retention, but may also increase ionic resistance and reduce gas permeability if not carefully controlled.
Electrolyte stratification—the accumulation of higher acid concentrations at the bottom of the battery—is a significant failure mode in VRLA batteries. The separator’s microstructure directly influences stratification by affecting acid-dripping speed and capillary forces . Separators designed to suppress stratification typically feature optimized pore size distributions and surface treatments that balance hydrophilic and hydrophobic properties.
Mechanical Strength and Dimensional Stability
AGM separators must withstand the mechanical stresses of battery assembly, plate expansion during cycling, and vibration in automotive applications. Tensile strength in the machine direction typically ranges from 0.3 to 1.2 kN/m for commercial products, with cross-direction strength somewhat lower . Elongation at break ranges from about 1% to 3% .
For demanding applications such as start-stop batteries and industrial cycling, separators with higher tensile strength and better dimensional stability are essential. Some manufacturers enhance mechanical properties through polymer emulsion treatments that create bonds at fiber contact points, increasing tensile strength by 25-50% while maintaining porosity . These modified AGM (MAGM) separators also exhibit improved chemical and thermal stability.
Advanced Considerations for Specialized Applications
High-Power and Start-Stop Applications
Automotive start-stop batteries represent one of the most demanding AGM applications. These batteries must deliver high cranking currents while enduring frequent partial-state-of-charge cycling. The separator must exhibit low electrical resistance to support high-rate discharge, typically achieved through optimized pore structure and minimal thickness . Additionally, the separator must maintain compression despite the mechanical stresses of engine compartment vibration and thermal cycling.
For these applications, separators with basis weights in the range of 80-160 g/m² and thicknesses of 0.5-1.1 mm are commonly specified . Lower electrical resistance is a key performance differentiator, with leading suppliers achieving values below 0.5 mΩ·dm² in compressed state .
Industrial and Stationary Applications
Industrial batteries for UPS, telecommunications, and renewable energy storage prioritize cycle life and reliability over power density. These applications typically use thicker AGM separators (1.0-2.8 mm) that provide larger electrolyte reservoirs and higher compression forces .
For tall stationary cells, maintaining uniform electrolyte distribution over the full plate height is challenging. Separators with micro-structural designs that suppress stratification are particularly valuable in these applications . Some manufacturers offer composite separators combining AGM layers with microporous polyolefin membranes for enhanced dendrite resistance and mechanical strength .
Deep-Cycle and Renewable Energy Storage
Deep-cycle applications, including renewable energy storage and motive power, subject separators to repeated charge-discharge cycles with significant plate volume changes. The separator’s elastic recovery—its ability to rebound after compression—becomes critical for maintaining plate contact over thousands of cycles .
Separators for deep-cycle applications should exhibit high wet elasticity and minimal compression set. Higher fine fiber content improves these properties but may compromise acid filling speed. A balanced formulation with optimized fiber blending is essential.
Supplier Selection and Quality Considerations
Choosing the right AGM separator involves not only technical specifications but also supplier capability and quality systems. The AGM separator market is relatively concentrated among established international manufacturers, with production reaching approximately 1,058 million square meters globally in 2025 .
Supplier selection criteria should include production consistency, as micro-variations in thickness, permeability, and pore structure can significantly affect battery performance . Leading suppliers invest in fiber control and web formation technologies to deliver tight tolerances and uniform product quality. Vertical integration—from glass composition control to finished roll conversion—is a hallmark of the most reliable suppliers .
Technical service capability is another important differentiator. Suppliers that can assist with separator selection, compression optimization, and troubleshooting electrolyte wetting issues help battery manufacturers reduce time-to-market and improve production yields . Given that qualification timelines for new separator grades can extend for months, establishing strong supplier partnerships is strategically important.
Conclusion
Selecting the right AGM separator for VRLA batteries requires balancing multiple, sometimes competing, requirements: high porosity for electrolyte retention versus adequate gas permeability for oxygen recombination; fine fibers for capillary pressure versus coarse fibers for acid filling speed; thin profiles for power density versus thick profiles for cycle life. The optimal choice depends on the specific application, duty cycle, and manufacturing constraints.
Battery designers should work closely with separator suppliers from the earliest stages of cell development, treating the separator as a strategic subsystem rather than a commodity input. By understanding the fundamental relationships between fiber composition, pore structure, and battery performance, engineers can make informed decisions that enhance capacity, extend cycle life, and ensure reliable operation across diverse operating conditions.
As the energy storage landscape evolves, AGM separators continue to advance through improved fiber engineering, novel binder systems, and composite structures. Staying informed about these developments and maintaining rigorous incoming quality control will be essential for manufacturers seeking to maintain competitive advantage in the increasingly demanding VRLA battery market.
Post time: Oct-15-2026


